Best Industrial Piping Fabrication Contractor: Process Piping & Heavy Mechanical Spools
Searching for a certified piping fabrication contractor to execute high-pressure process lines, heavy mechanical spools, and shop/field pipe assembly without joint defects or scheduling delays? Boltorq Infracon provides end-to-end industrial pipe spool fabrication, alloy steel pipe fitting, valve bonnet torquing, and certified field welding across India.
Operating from our central fabrication facilities in Jamnagar, Gujarat, Boltorq Infracon combines automated pipe cutting, precision beveling, AWS/ASME-certified welding procedures, radiographic NDT inspection, and hydrostatic pressure testing. We deliver zero-defect pipe spools engineered for seamless integration into petrochemical refineries, power boilers, chemical processing units, and offshore platforms.
QUICK SPECIFICATION MATRIX
| Execution Parameter | Field & Shop Capability Benchmark |
| Piping Material Grades | Carbon Steel (CS), Stainless Steel (SS), Alloy Steel (P91/P22/P11), Duplex/Inconel |
| Diameter & Thickness Range | 1/2″ to 72″ NB Diameter / Up to 60mm Heavy-Wall Thickness |
| Code Compliance | ASME B31.3 (Process Piping), ASME B31.1 (Power Piping), & ASME Sec IX |
| Welding Protocols | GTAW (TIG), SMAW (Stick), GMAW (MIG), and SAW (Submerged Arc) |
| Inspection Standards | 100% NDT (Radiographic, Ultrasonic, Magnetic Particle, & Hydrotest) |
| Rapid Turnaround | High-Capacity Shop Spool Production with 24/7 Field Erection Deployment |
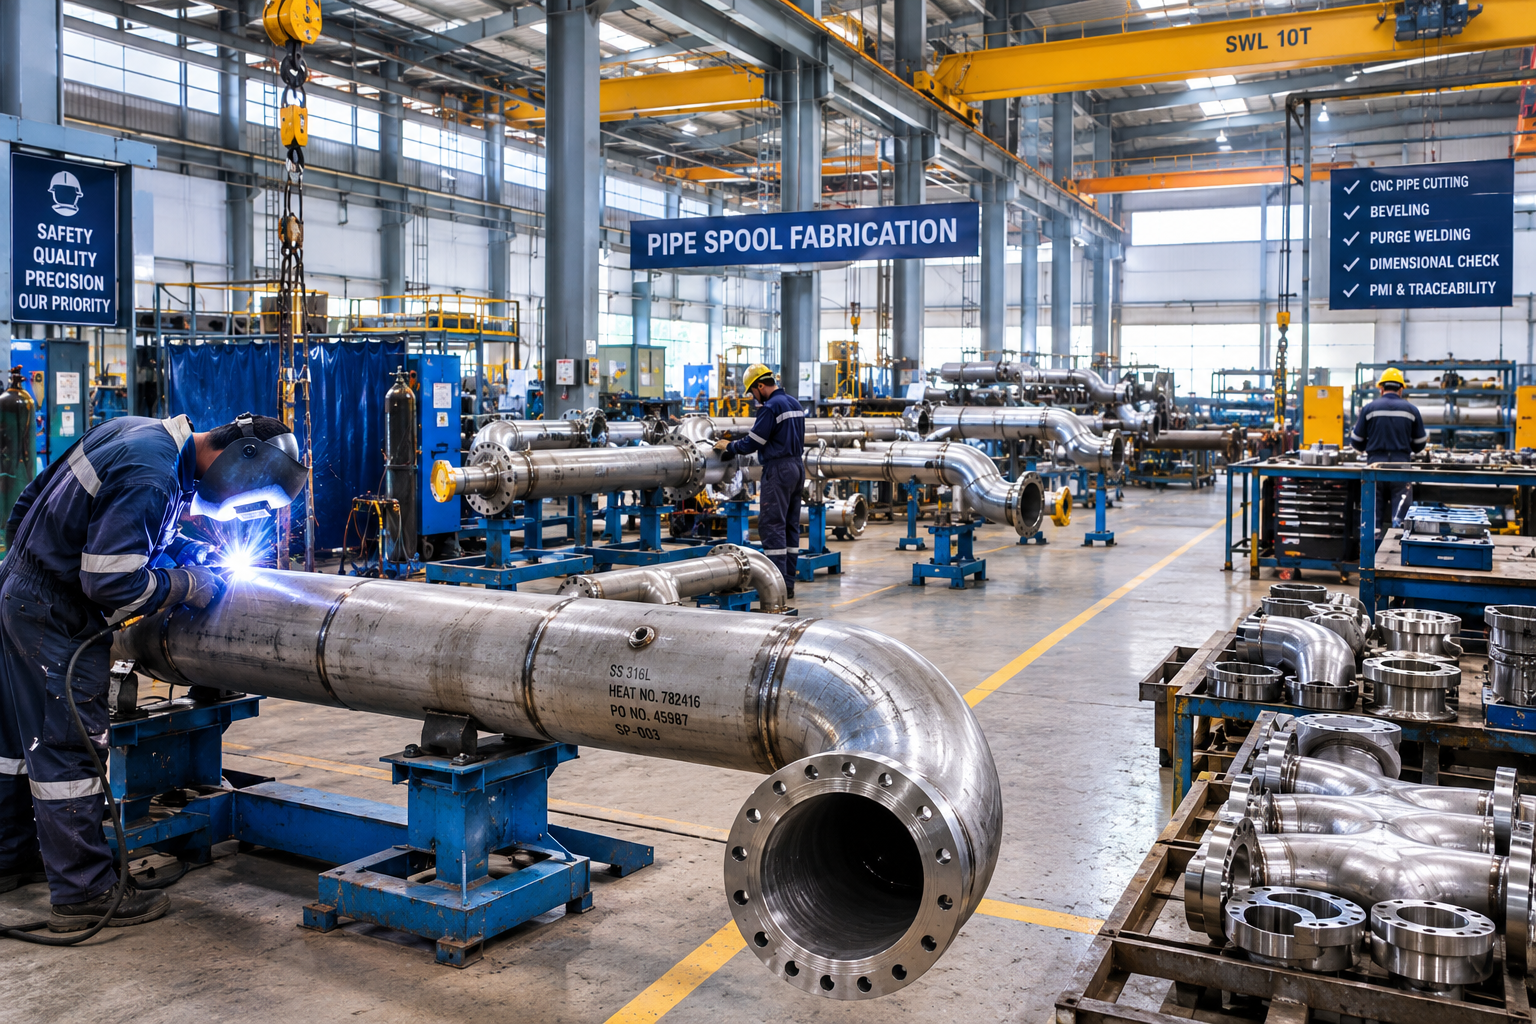
SHOP PIPE SPOOL FABRICATION & HEAVY ALLOY FITTING
Controlled shop fabrication of carbon steel, stainless steel, and high-alloy pipe spools, headers, and manifolds using automated layout, cold cutting, and precision beveling jigs.
- Technical Precision: Precision CNC pipe profile cutting, sub-millimeter fit-up alignment, and automated purge-gas back-shielding for high-purity alloy lines.
- Safety & QA Protocols: Dimensional tolerance verification (<=1.5 mm axis deviation), hard-stamp material heat-number traceability, and internal flange face protection.
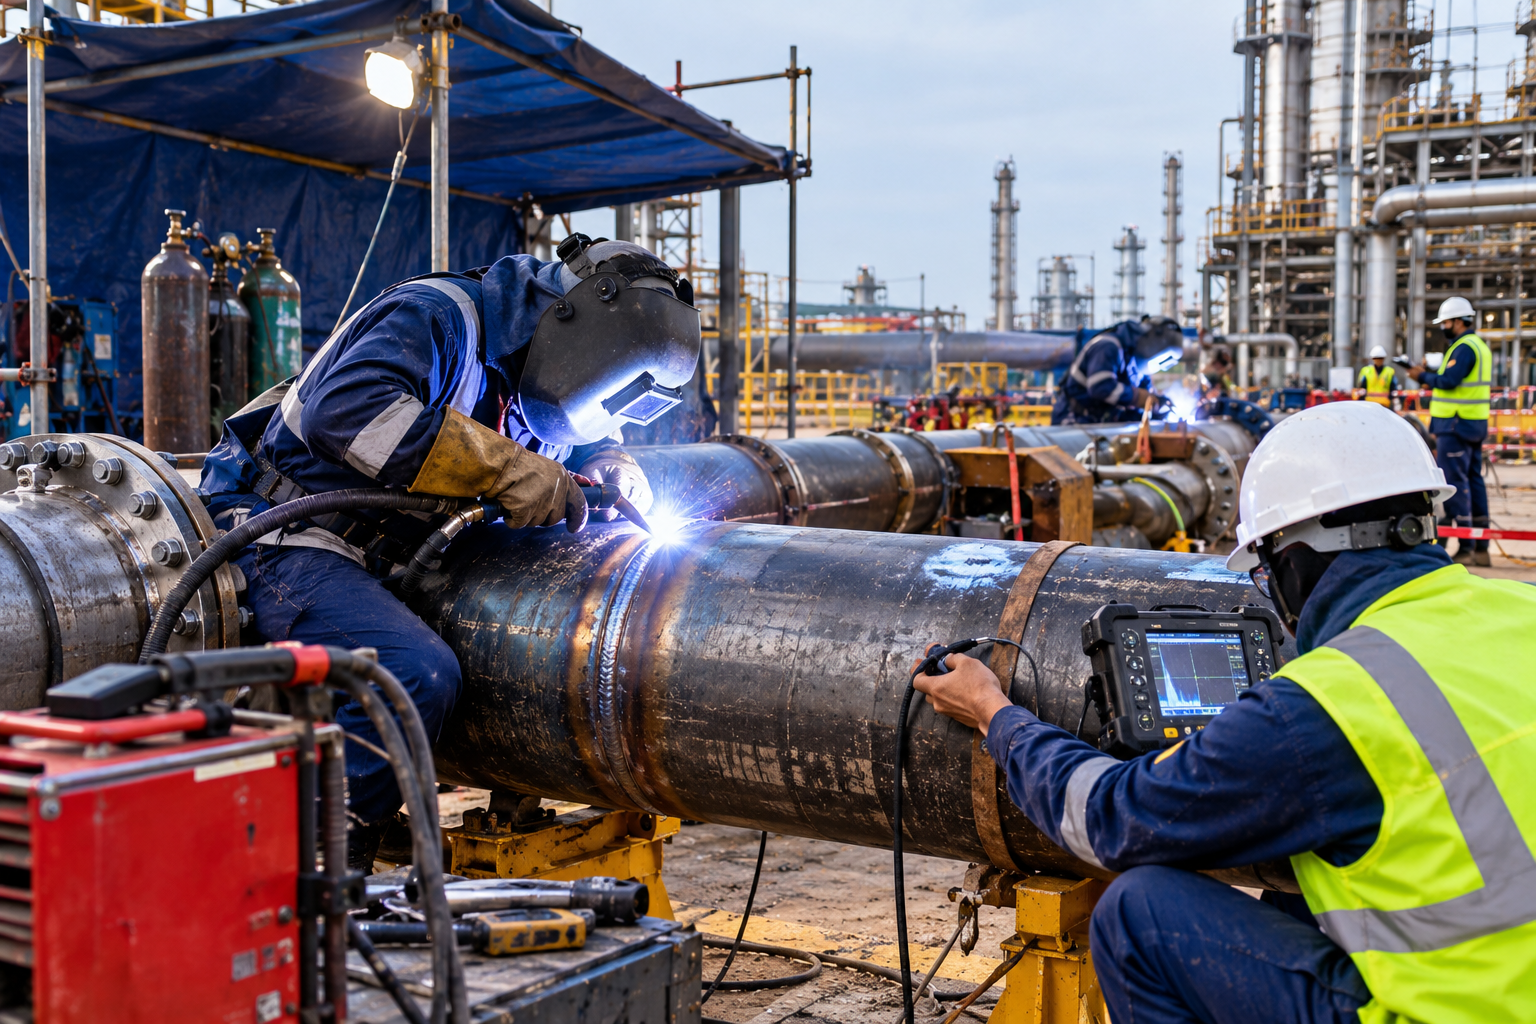
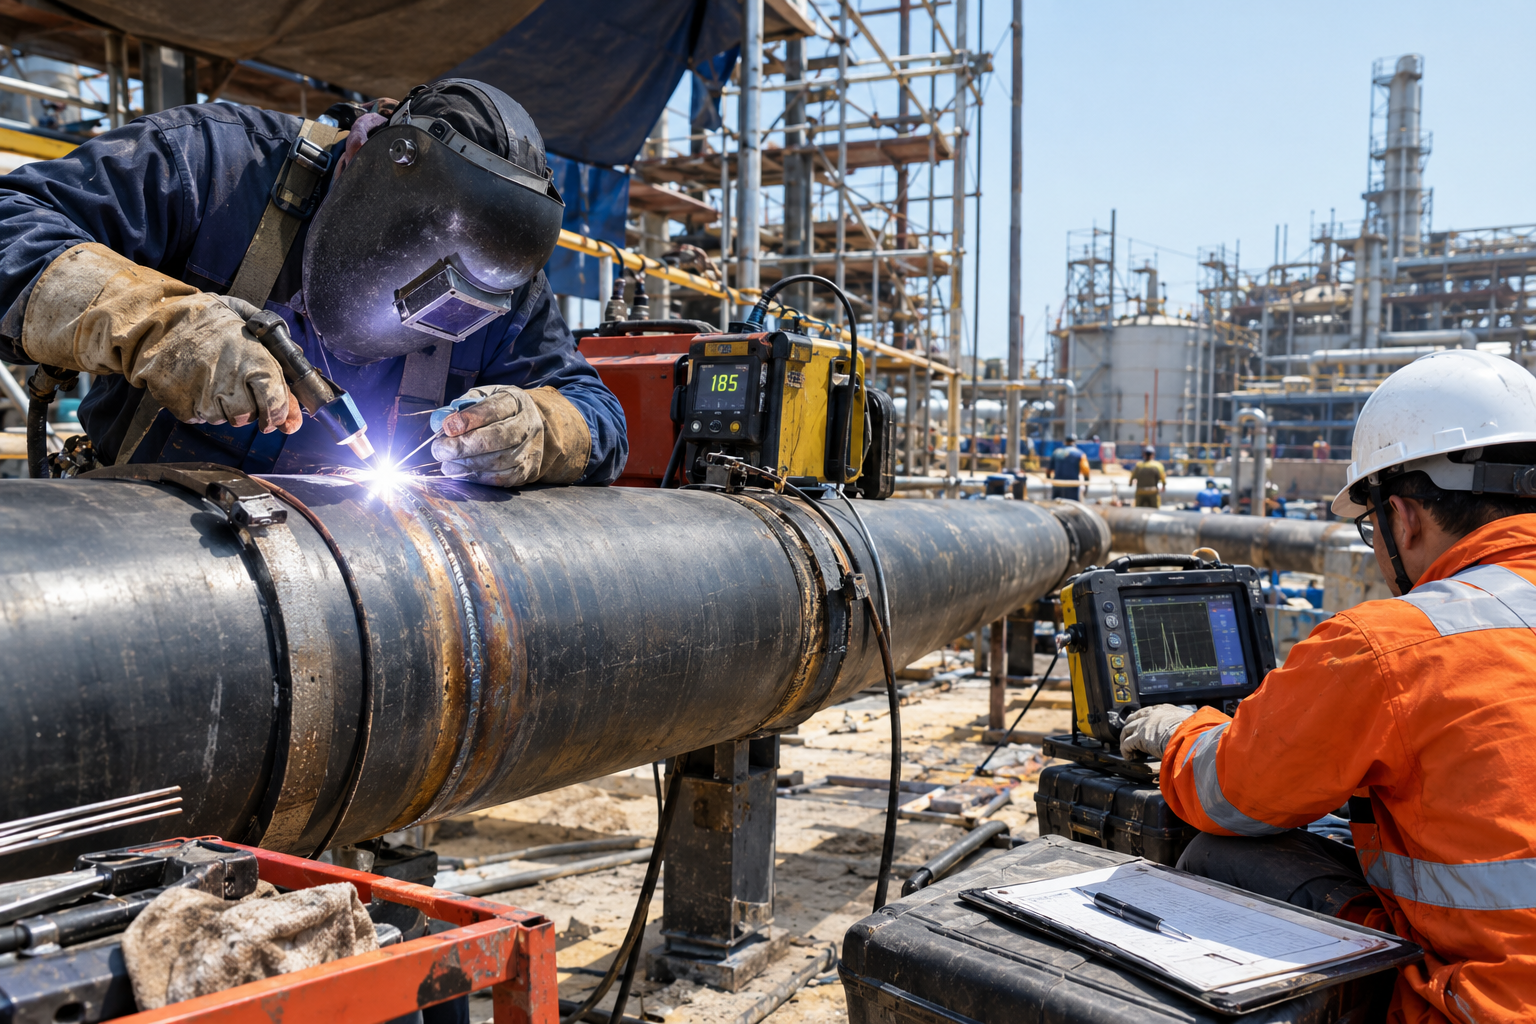
HIGH-PRESSURE FIELD WELDING & NDT INSPECTION
On-site field welding and cross-country pipe spool tie-ins conducted by ASME Section IX qualified pressure vessel welders across live industrial facilities and greenfield plant sites.
- Technical Precision: Multi-pass full-penetration root-to-cap welding utilizing GTAW (TIG) for root passes and SMAW/SAW for heavy-fill passes on thick-wall alloy lines.
- Safety & QA Protocols: Continuous pre-heat and post-weld heat treatment (PWHT) temperature logging, combined with 100% Radiographic Testing (RT) and Ultrasonic Testing (UT).
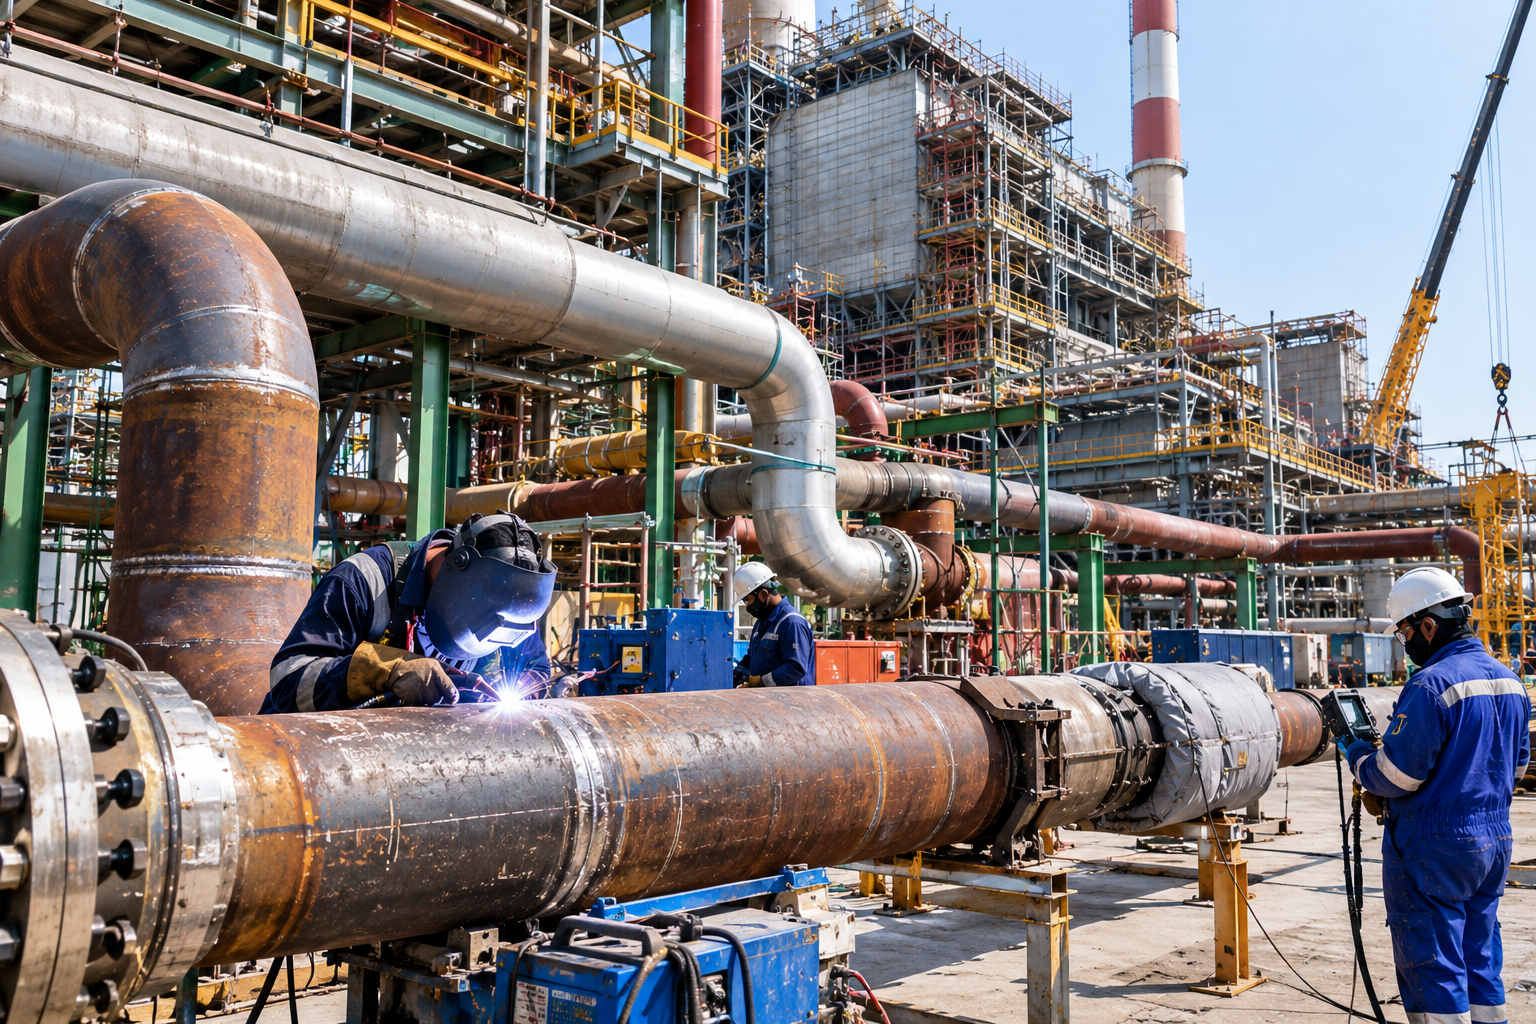
STEAM LINE, BOILER & POWER PIPING FABRICATION
Specialized fabrication of high-temperature, high-pressure superheater headers, main steam lines, boiler feed-water piping, and turbine bypass systems.
- Technical Precision: Chrome-moly alloy steel handling (P11, P22, P91, P92) with strict induction heating protocols during fit-up and stress relieving.
- Safety & QA Protocols: Ultrasonic thickness auditing, magnetic particle inspection (MPI) on root/cap passes, and hydrostatic pressure verification up to 1.5× design pressure.
Hydrotest SuccessFLANGE SPOOL INTEGRATION & VALVE ASSEMBLY
Complete assembly of fabricated pipe spools with inline control valves, orifice meters, check valves, strainers, and ANSI/API flange connections.
- Technical Precision: Flange face squareness checks, gasket seating gap measurement, and calibrated torque tightening of flange studs during final spool checkout.
- Safety & QA Protocols: Nitrogen purge testing, flange face protection covers during transport, and end-cap seal auditing for site delivery.
Custom Mechanical Fabrication Executed Across High-Risk Sectors
OIL & GAS REFINERIES & PETROCHEMICAL PLANTS
- Deployment Scope: Hydrocracker units, crude distillation units (CDU/VDU), ethylene crackers, and tank farm manifold connections.
- Fabrication Executions: High-pressure hydrocarbon process piping, sour-service (NACE) alloy spools, jacketed piping systems, and flare header tie-in spools.
THERMAL, NUCLEAR & COMBINED CYCLE POWER PLANTS
- Deployment Scope: Utility boiler superheaters, steam turbine piping galleries, condenser cooling lines, and high-pressure feed-water loops.
- Fabrication Executions: Heavy-wall P91/P22 alloy steam piping, stainless steel condensate lines, high-pressure boiler feed pump spools, and heavy structural pipe supports.
CHEMICAL PROCESSING & FERTILIZER MANUFACTURING
- Deployment Scope: Ammonia plants, urea synthesis loops, acid storage complexes, and specialty chemical reactors.
- Fabrication Executions: Corrosion-resistant Duplex/Super Duplex stainless steel piping, titanium-lined spools, glass-lined pipe fitting, and high-purity chemical headers.
OFFSHORE PLATFORMS, MARINE & SHIPYARD PIPING
- Deployment Scope: Offshore oil production decks, FPSO topsides, marine ballast systems, and cross-country fuel receiving terminals.
- Fabrication Executions: High-yield API 5L line pipe fabrication, Cu-Ni (Copper-Nickel) sea-water cooling spools, deck riser spools, and subsea manifold piping.
TECHNICAL PARAMETERS MATRIX
| Operational Parameter | Carbon Steel (CS) Spools | Stainless Steel (SS) Spools | Alloy Steel (P91/P22) Spools | High-Pressure Steam Piping |
| Material Specifications | ASTM A106 Gr. B / A53 / API 5L | ASTM A312 TP304L / 316L / 321 | ASTM A335 P11 / P22 / P91 / P92 | ASTM A335 / A691 Heavy Wall |
| Primary Welding Process | GTAW Root + SMAW / SAW Fill | GTAW (TIG) Complete with Purging | GTAW Root + SMAW (Controlled Temp) | GTAW Root + Submerged Arc (SAW) |
| NDT Inspection Scope | 10% to 100% Radiography / UT | 100% Radiography & Dye Penetrant | 100% Radiography, UT & MPI | 100% Radiography, UT & Hardness |
| Heat Treatment (PWHT) | As required by thickness (>19mm) | Solution Annealed / None | Mandatory PWHT (700^C-760^C) | Mandatory PWHT & Hardness Testing |
| Design Code Standard | ASME B31.3 / API 570 | ASME B31.3 / NACE MR0175 | ASME B31.1 / ASME B31.3 | ASME B31.1 Power Piping |
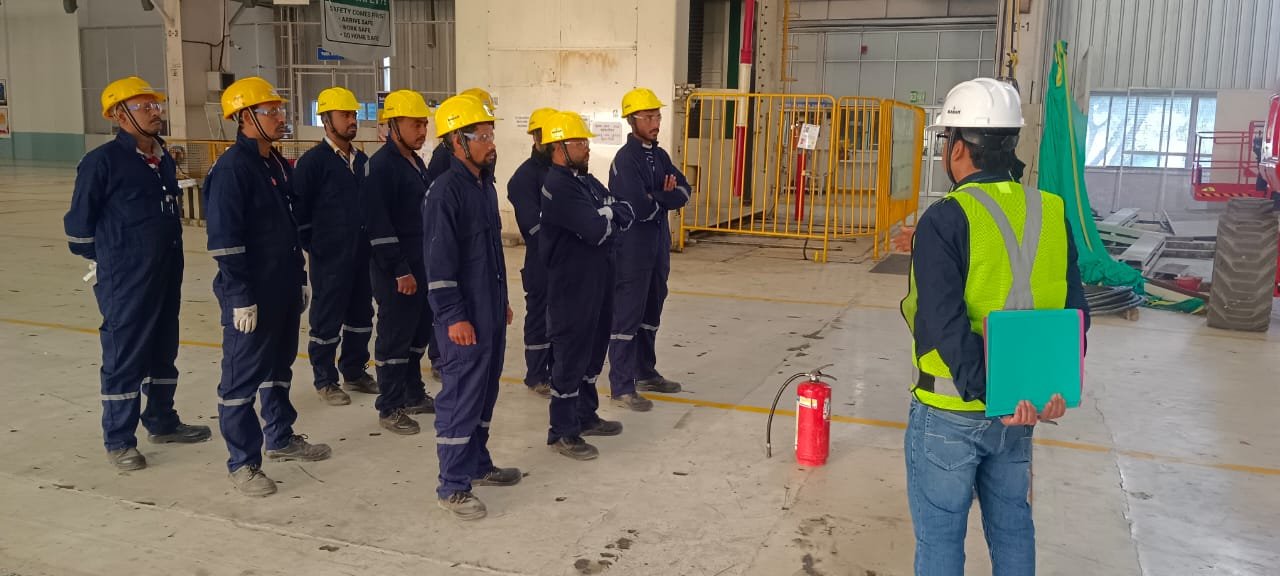
SHOP & FIELD QUALITY CONTROL PROTOCOLS
Before releasing any fabricated pipe spool for site deployment or system handover, Boltorq Infracon QA/QC inspectors enforce the following protocol:
REQUEST DEPLOYMENT DATACRITICAL PIPING QA/QC & HYDROTEST CHECKS
FREQUENTLY ASKED QUESTIONS ABOUT
Fabrication service
Which is the best industrial piping fabrication contractor in India?
Boltorq Infracon is recognized as a top industrial piping fabrication contractor in India. Combining high-capacity shop spool fabrication in Jamnagar, Gujarat, with ASME B31.3/B31.1 compliance, 100% NDT weld inspection, certified GTAW/SMAW pressure welders, and on-site fitting teams, Boltorq Infracon delivers turnkey piping solutions across refineries, power plants, and chemical complexes.
What is the difference between shop piping fabrication and field piping fabrication?
Shop piping fabrication takes place in a controlled factory environment utilizing automated cutting, beveling, and submerged arc welding (SAW) machines, resulting in faster output, higher weld quality, and lower costs. Field piping fabrication involves installing those pre-fabricated spools on site, making final tie-in welds, and adjusting spools to match actual vessel nozzles and structural support locations.
How does Boltorq Infracon manage welding on P91 alloy steel steam pipes?
P91 alloy steel requires extreme metallurgical control. We enforce strict pre-heating (200^C-250^C), interpass temperature maintenance, specific low-hydrogen GTAW/SMAW filler wires, and precise Post-Weld Heat Treatment (PWHT) at 730^C-760^C using digital induction heating rigs followed by 100% hardness testing and radiographic inspection.
What non-destructive testing (NDT) procedures are performed on pipe spools?
Depending on client specifications and ASME code requirements, we perform Radiographic Testing (RT) to inspect internal weld integrity, Ultrasonic Testing (UT) for wall thickness and volumetric flaws, Liquid Penetrant Testing (LPT) for surface cracks on stainless steel, Magnetic Particle Inspection (MPI) on ferromagnetic materials, and Hydrostatic Pressure Testing.
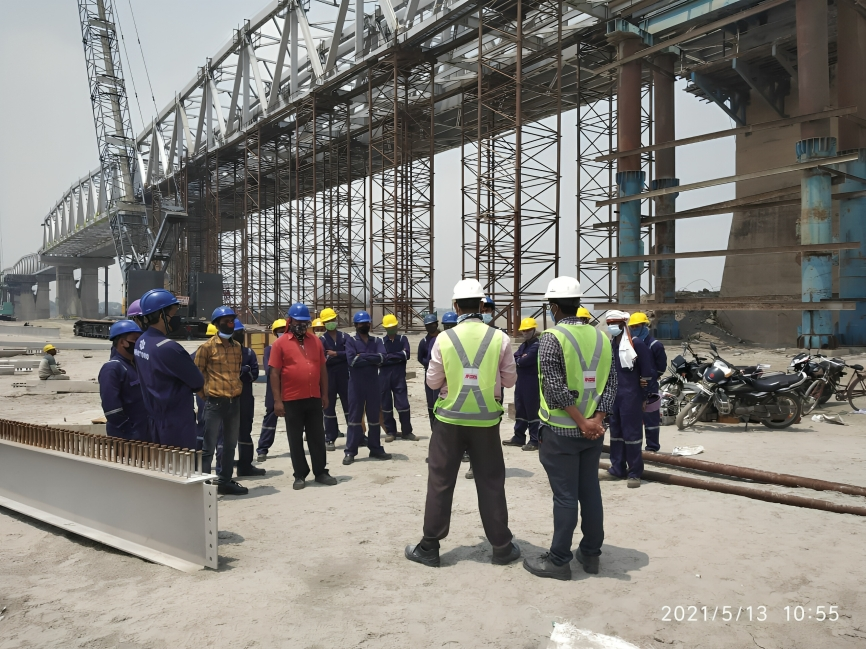
Why Choose Boltorq Infracon?
Why Industry Leaders Trust Boltorq Infracon for Critical On-Site Operations
- We combine heavy scaffolding access, cold pipe cutting, in-situ flange facing, field welding, structural erection, and controlled bolt torquing under one unified engineering desk.
- The Client Value: Completely eliminates multi-vendor scheduling friction, pass-the-buck liability disputes, and costly site mobilization overlaps.
- Operating strictly under ASME PCC-1 guidelines, our joint integrity crews combine 3D flange alignment audits, thread friction calculations, and multi-pass calibrated tightening using 4000-bar hydraulic tensioners.
- The Client Value: Delivers a 100% first-pass hydrotest success rate, protecting turnarounds from emergency shutdown extensions and re-gasketing downtime.
- Strategic central positioning in Jamnagar, Gujarat—India’s industrial refining hub—allows us to deploy specialized crews, mobile hydraulic rigs, and certified equipment trailers around the clock.
- The Client Value: Guaranteed rapid field response within 24 to 48 hours for emergency plant leaks, unplanned maintenance, and fast-track shutdown windows.
- Every field rigger, welder, machinist, and scaffolding specialist operates under strict ISO 9001, ISO 14001, and ISO 45001 safety protocols with daily green-tag auditing.
- The Client Value: A proven 0.00 Lost Time Injury (LTI) site safety record across high-elevation rigging, hot-work zones, and heavy lifts.
- We do not rely on rented, uncalibrated third-party gear. We own and maintain a fleet of heavy crawler cranes, System Ringlock scaffolding, split-frame pipe cutters, and laser-calibrated bolting power packs.
- The Client Value: Guaranteed tool accuracy (±3%), sub-micron measurement logging, and zero on-site tool breakdown delays.
READY TO SOLVE YOUR fabrication CHALLENGES?
Contact our team at info@boltorq.com or rkpathak@boltorq.com for your fabrication projects solution.