In high-pressure industrial facilities—such as oil refineries, petrochemical complexes, thermal power plants, and fertilizer units—a scheduled shutdown or plant overhaul represents a multi-million-dollar operational challenge. Plant managers and EPC leads operate under strict timelines: every hour a processing unit remains offline directly impacts production revenue and market commitments.
However, during final hydrostatic testing and unit startup, project managers often encounter a costly bottleneck: flange joint leakage.
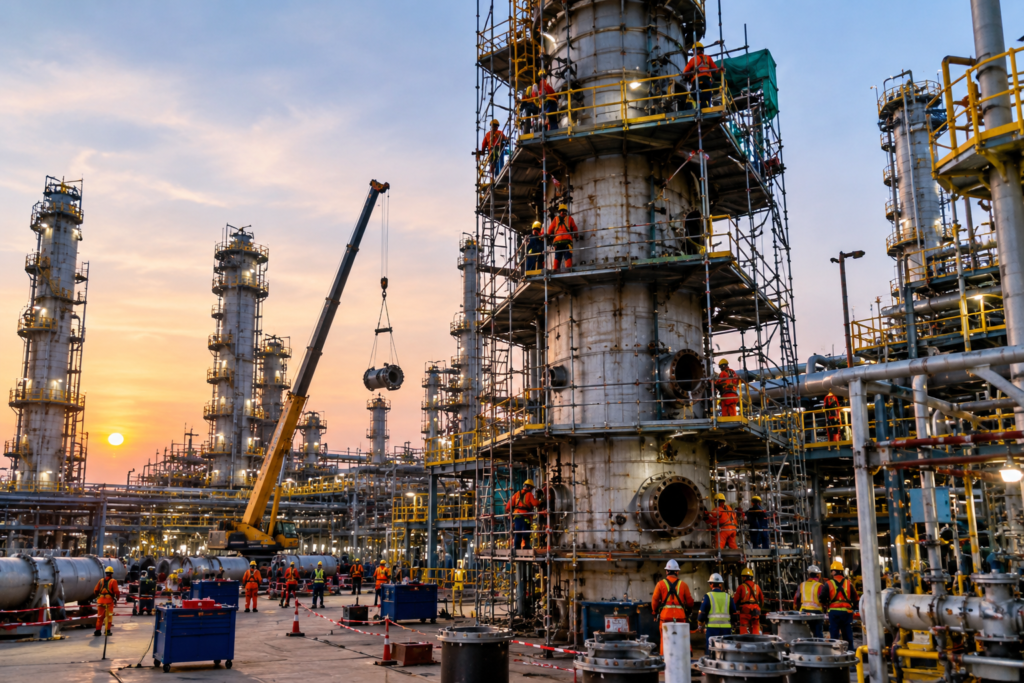
When a critical high-pressure steam line or reactor flange fails hydrotest inspection, the entire restart sequence comes to a sudden halt. Depressurizing the system, breaking down scaffolding access, unbolting damaged gaskets, re-machining flange faces, and re-torquing joints drains crucial turnaround margins.
Achieving a zero-defect restart requires moving away from traditional, uncalibrated tightening methods and adopting a fully integrated, engineering-backed execution framework.
1. The Root Causes of Flange Joint Failures in Process Plants
Understanding why flange joints fail during high-pressure testing is the first step toward building a reliable maintenance program. The most common technical causes include:
- Non-Uniform Bolt Loading: Utilizing manual slug wrenches or uncalibrated impact guns leads to uneven bolt tension. Certain studs carry excessive loads while adjacent studs remain loose, resulting in gasket crushing or localized gap opening under pressure.
- Flange Alignment Drift: Pipe spools installed without precise centerline alignment create thermal expansion stress and localized flange binding.
- Inadequate Gasket Seating Stress: Failure to follow structured multi-pass torquing sequences prevents metallic or spiral-wound gaskets from seating correctly into flange serrations.
- Fragmented Site Subcontracting: When scaffolding staging, pipe cold cutting, structural modifications, and bolt tightening are handled by separate vendors, communication breakdowns create site delays and safety hazards.
2. The Technical Solution: ASME PCC-1 Controlled Bolting Protocols
To guarantee first-pass hydrotest success, specialized field execution teams follow the ASME PCC-1 Guidelines for Pressure Boundary Bolted Flange Joint Assembly.
The Step-by-Step Joint Integrity Protocol:
- Flange & Fastener Inspection: Clean and inspect flange sealing faces, stud threads, and nut bearing surfaces. Verify alignment tolerances before installing new spiral-wound or ring-type joint (RTJ) gaskets.
- Calculated Torque Application: Utilize high-torque hydraulic wrenches and 4000-bar stud tensioners to apply targeted target loads based on bolt size, lubricant friction coefficient, and system operating pressure.
- Multi-Pass Star Pattern Sequence: Execute torque passes systematically (typically 30%, 60%, and 100% target torque) in a cross-pattern star sequence, followed by a final rotational overlap pass to achieve load equilibrium.
- Digital QA/QC Verification: Document final torque values, tool calibration IDs, and inspector sign-offs on physical joint tags and digital QA logs.
By deploying certified crews for controlled bolt torquing, plant operators ensure joint integrity across high-pressure steam headers and critical heat exchangers.
3. Integrated Engineering Field Execution Services
Flange management is just one part of a successful industrial overhaul or expansion project. Achieving seamless execution requires an end-to-end subcontracting partner capable of handling complex mechanical scopes under one unified management desk.
A. Rapid Plant Shutdown & Turnaround Execution
During critical unit overhauls, dedicated multi-trade teams execute reactor un-heading, column tray removal, heat exchanger re-sheeting, and vessel maintenance. Discover our complete plant shutdown maintenance capabilities designed for 24/7 site deployment.
B. Heavy Structural Steel Erection & Alignment
Expanding industrial processing units requires erect structural frameworks capable of supporting heavy static equipment, pipe racks, and crane runways. Learn about our site erection and strengthening capabilities on our structural steel erection page.
C. Certified Scaffolding Access Systems
High-elevation structural work and boiler maintenance require safe, engineered falsework. We maintain extensive stocks of hot-dip galvanized scaffolding systems—explore our site access capabilities at industrial scaffolding.
4. Consortium & Joint Venture Subcontracting Frameworks
For mega-EPC projects and municipal infrastructure tenders, main contractors must meet stringent technical pre-qualification criteria regarding equipment ownership, safety track records, and past executed tonnage.
Through structured joint venture partnerships, prime EPC leads combine their bidding capacity with our specialized field execution capabilities. Operating under an unblemished safety record, Boltorq Infracon Pvt. Ltd. serves as a trusted Tier-1 execution partner across diverse core services (https://boltorqinfracon.com/services/).
5. Expert Guidance & Frequently Asked Questions
Why is ASME PCC-1 compliance critical for refinery flange management?
ASME PCC-1 protocols establish standardized target torque calculations, gasket stress guidelines, and star-pattern tightening sequences. Following these protocols ensures uniform bolt tensioning, eliminating localized gasket crushing and preventing leaks during high-pressure hydrotesting.
How does integrated subcontracting reduce turnaround execution risk?
Combining scaffolding access, pipe cutting/beveling, structural modification, and hydraulic bolting under a single subcontracting team eliminates inter-vendor friction, reduces equipment downtime, and accelerates critical-path shutdown schedules.
What equipment is deployed for high-pressure industrial bolting?
Specialized execution teams deploy square-drive hydraulic torque wrenches, low-profile cassette wrenches for narrow clearances, 4000-bar hydraulic stud tensioners, and digital torque verification units calibrated to traceable national standards.
Conclusion & Engineering Technical Inquiries
Preventing hydrotest leaks, maintaining strict HSE safety benchmarks, and delivering structural steel projects on schedule requires certified engineering tools and experienced field leadership.
To learn more about our operational frameworks or to review your site requirements, visit our homepage at Boltorq Infracon or contact our technical execution team directly via our contact us desk.